
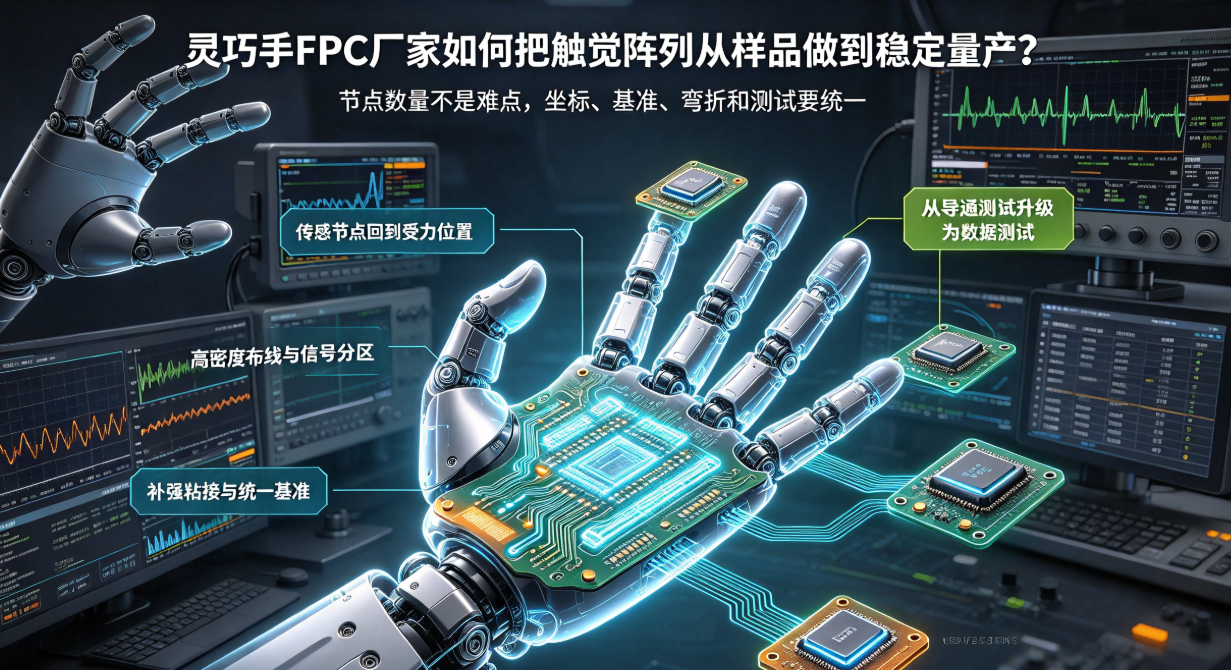
Tactile arrays for dexterous hands feature numerous sensing nodes in confined spaces—and must endure repeated finger motion. Signal acquisition in prototypes does not guarantee stable mass production. This article outlines how FPC manufacturers establish a closed-loop mass production process, covering sensor node layout, dynamic zoning, reinforcement positioning, test calibration, and batch data management.
The core challenge in mass-producing tactile arrays is not the sheer number of nodes.
Dexterous hand FPCs must aggregate multi-channel tactile signals from fingertips, palmar surfaces, and joints to the control unit. While higher node counts increase trace density and interconnect complexity, the true bottleneck for mass production lies in early alignment of node coordinates, assembly datums, dynamic bending zones, and test methodologies.
Sensing nodes must be positioned at actual load-bearing locations.
During design, overlay finger geometry, sensor footprints, datum holes, bonding surfaces, and load-bearing regions for verification. Node misalignment relative to the load center degrades data consistency; mechanical stretching of traces within the sensing zone introduces baseline drift. Keep the sensing zone structurally stable; confine primary bending to designated dynamic zones with adequate margin and predictable trajectories.
High-density routing must not compromise signal integrity.
Separate analog tactile traces from motor, power, and high-speed communication lines. Use ground guards or shielding where necessary. Connector pin assignments must account for crosstalk sensitivity among adjacent channels. Even in dense routing areas, maintain sufficient process windows—avoid relying on edge-case parameters that pass in prototypes but cause instability in mass production.
Reinforcement, bonding, and fixturing are interdependent elements.
Reinforcement stabilizes connectors and pads—but if its boundary overlaps the dynamic zone, it creates stress concentration. Bonding surface position, thickness, and pressure must be tightly controlled to prevent preloading the sensor. Assembly fixtures must reference a unified datum to ensure consistent node placement across batches.
Mass-production testing must evolve from simple 'continuity' checks to full 'data-driven' validation.
- Record trace resistance, insulation resistance, and status of all channels prior to assembly.
- Post-assembly, capture no-load baselines, output under specified loads, and noise profiles.
- After bending or grasp cycling, compare drift, hysteresis, and anomalous channel behavior.
- Log temperature, batch ID, material lot, and test fixture ID to enable full traceability.
What capabilities bridge the gap from prototype to mass production?
Dexterous hand FPC manufacturers must integrate expertise in fine-line circuitry, dynamic mechanical structures, sensor signal conditioning, and assembly-level testing. Hongyi Precision engages early in 3D structural and sensor layout reviews, converges reinforcement, bonding, and electrical test parameters via prototypes and small-batch runs, and translates validated test data into definitive mass-production acceptance criteria.