
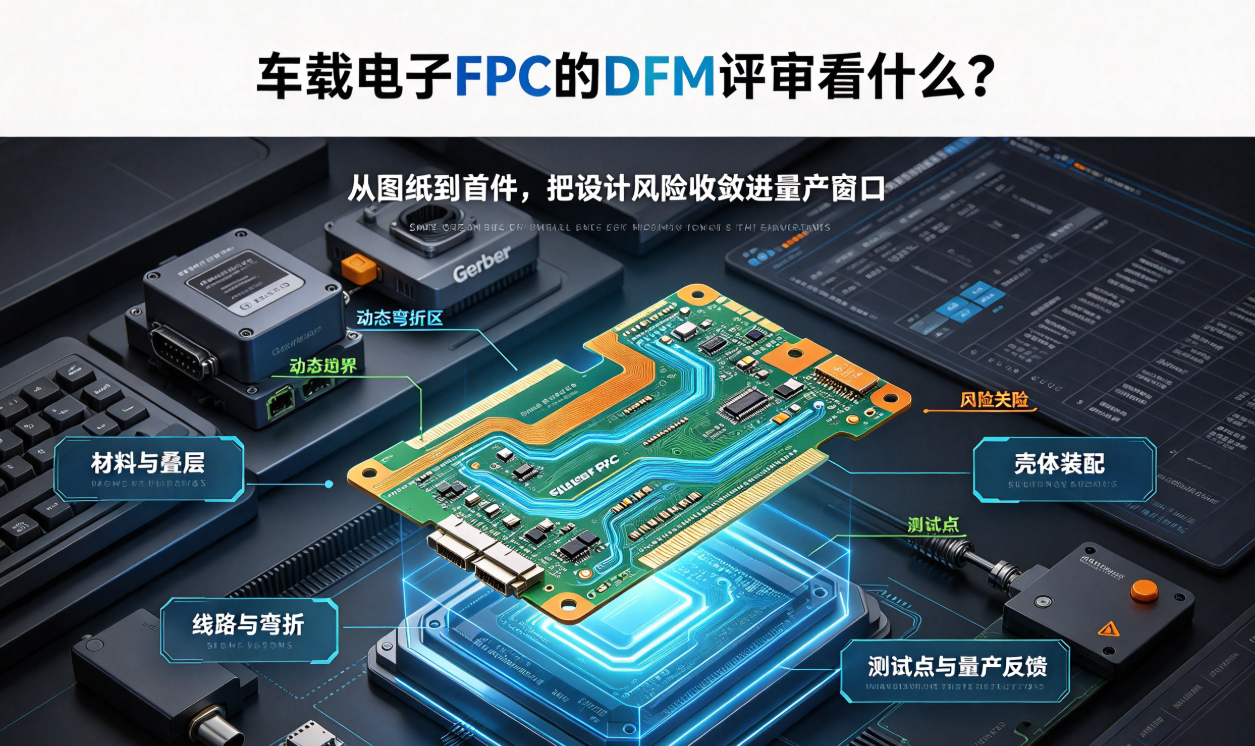
The most valuable step before mass production of automotive FPCs is DFM review. Proactively verifying materials, stack-up, trace width/spacing, flex zones, pads, connectors, and test points—before tooling and trial runs—uncovers the majority of high-cost risks. This article presents a first-article review framework tailored for automotive projects.
The goal of DFM review is to transform drawings into stable, producible products.
For automotive FPC projects, discovering insufficient bend clearance, stiffener interference, or missing test points only after sample fabrication often impacts structural components, connectors, and delivery schedules simultaneously. The value of DFM lies in translating design intent—during the drawing phase—into executable parameters for materials, processes, and assembly, and explicitly identifying dimensions requiring joint confirmation by supplier and customer.
An effective review record should not simply state 'manufacturable'; it must specify risk locations, recommended modifications, verification methods, and responsibility boundaries.
I. Materials and Stack-Up: Confirm Operating Environment First
Material review for automotive FPCs begins with operating temperature, thermal cycling, vibration, humidity-heat exposure, and mounting method. Substrate, copper foil, coverlay, adhesive system, and stiffeners must form a matched combination—not a direct substitution from standard consumer-electronics materials. For high-temperature zones, display modules, or dynamic flex areas, confirm how material CTE and flexibility affect dimensional stability and service life.
II. Traces and Flex Zones: Trace Stress Pathways
Trace review covers more than just trace width/spacing, hole diameter, and layer count—it also verifies whether routing follows the actual bending direction, whether vias and pads avoid the neutral bend axis, and whether branches concentrate within the same cross-section. When entering connector or stiffener zones, design a continuous stiffness transition to prevent abrupt shifts from 'flexible' to 'hard-bend'.
- Dynamic Zone: Prioritize minimum bend radius, trace continuity, and copper stress relief.
- Static Zone: Locate connectors, tooling holes, test points, and larger pads.
- Transition Zone: Control stiffener edge placement, adhesive layer thickness, and housing clamping force to prevent stress concentration.
III. Assembly: Incorporate Housing Tolerances into Review
Clearance in flat state does not guarantee trouble-free assembly into the housing. DFM review must overlay tolerances from clips, foam pads, screws, connector mating forces, and adjacent parts—checking for pinching, pulling, interference, or insufficient bend radius. Tooling holes and datum edges must align with assembly fixtures; non-compressible zones should be explicitly defined on drawings when necessary.
IV. Testability: No Test Points Means No Reliable Production Feedback
Automotive projects must plan electrical test fixtures, probe contact surfaces, optical inspection zones, and critical dimension datums during FPC design. For high-speed or sensitive signals, verify feasibility of impedance, insulation resistance, DC resistance, and functional testing. Test points that are too small, obscured by stiffeners, or interfered with by housings weaken production testing—making it overly reliant on manual judgment.
From Review Conclusion to First-Article Confirmation
- Label each risk location with design requirements, process capabilities, and assembly constraints.
- Convert trace width/spacing, hole diameter, stiffener tolerance, outline dimensions, and bend radius into first-article inspection items.
- Produce samples using near-production materials, equipment, and fixtures to avoid disconnect between sample conditions and mass production.
- Define clear pass/fail criteria for functional performance after thermal cycling, vibration, flexing, and component placement.
Hongyi Precision engages early in automotive FPC projects—participating in drawing and 3D assembly reviews—to provide actionable feedback on manufacturability, reliability, and delivery timing. We then validate design risk mitigation through first-article and small-batch builds, converging residual risks into the mass-production window.