
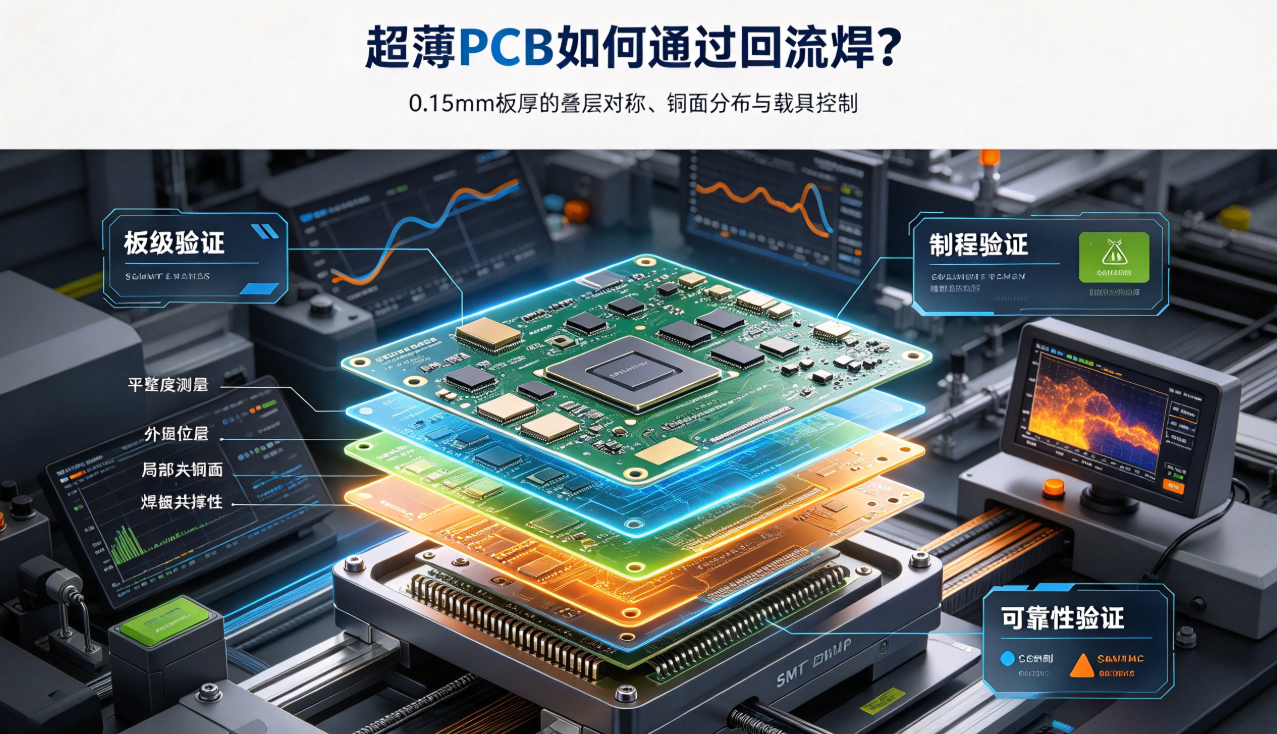
When ultra-thin PCBs enter SMT, warpage during reflow soldering, solder paste printing stability, and component placement accuracy become new challenges. A 0.15 mm board thickness is not simply a scaled-down version of conventional PCBs—it requires redefining the process window from stack-up symmetry and copper distribution to carrier support, thermal profile, and inspection methodology.
Why does SMT become more sensitive at 0.15 mm?
Ultra-thin PCBs resolve module height and mechanical space constraints—but reduced board stiffness increases susceptibility to flexure during reflow soldering, handling, and placement. Even minor surface deformation can compromise stencil contact, solder paste transfer, component placement accuracy, and solder joint coplanarity. For applications requiring high-Tg materials or automotive use, additional demands for thermal shock resistance and dimensional stability further complicate processing.
Therefore, 0.15 mm ultra-thin PCBs must adopt an SMT-driven approach—designing stack-up and lamination backward from assembly requirements—not waiting until placement defects occur before corrective action.
Stack-up symmetry is the foundation of planarity control.
Significant asymmetry in top/bottom materials, copper thickness, or pattern distribution leads to differential shrinkage during lamination and cooling. Designers should balance copper distribution across layers, verify dielectric thickness and stiffener placement, and consider thin-board-specific carriers and support structures. Layer count, hole size, and trace resolution for 0.15 mm boards require independent evaluation—standard rules for 0.8 mm boards do not apply directly.
Copper distribution and large copper areas must be evaluated together.
Large copper planes reduce resistance but significantly increase local rigidity and thermal mass. Edges of copper pours, dense pad arrays, and large solder mask openings all contribute to uneven thermal distribution. Adjusting copper fill patterns, routing segmentation, and pad geometry helps achieve more uniform heating and contraction during lamination and reflow.
Thin-board carriers are not optional accessories.
During reflow, ultra-thin boards require stable mechanical support to maintain pad planarity. Carrier positioning, support point layout, temperature resistance, and cleanliness directly impact placement outcomes. Carrier design must avoid components, connectors, and localized high points while preventing board slippage during entry, transit, and cooling through the oven. Near-production carriers should be used during prototype validation to uncover assembly issues early.
We recommend validating reflow in three tiers:
- Board-level validation: Measure bare-board planarity, outline dimensions, and critical pad coplanarity.
- Process validation: Confirm solder joint appearance and placement offset under combined printing, placement, reflow profile, and carrier conditions.
- Reliability validation: Subject post-reflow boards to thermal cycling, bending, or assembly testing to monitor dimensional and electrical performance changes.
Hongyi Precision’s 0.15 mm / 0.2 mm ultra-thin FR4 PCBs support thin-board-specific lamination, high-Tg materials, LDI-fine-line patterning, and full delivery—from engineering evaluation to volume production. For ultra-thin PCB projects requiring SMT, we recommend providing component layout, pad data, and reflow process specifications concurrently during initial board release—to prevent conflicting optimizations between mechanical structure, PCB design, and assembly.