
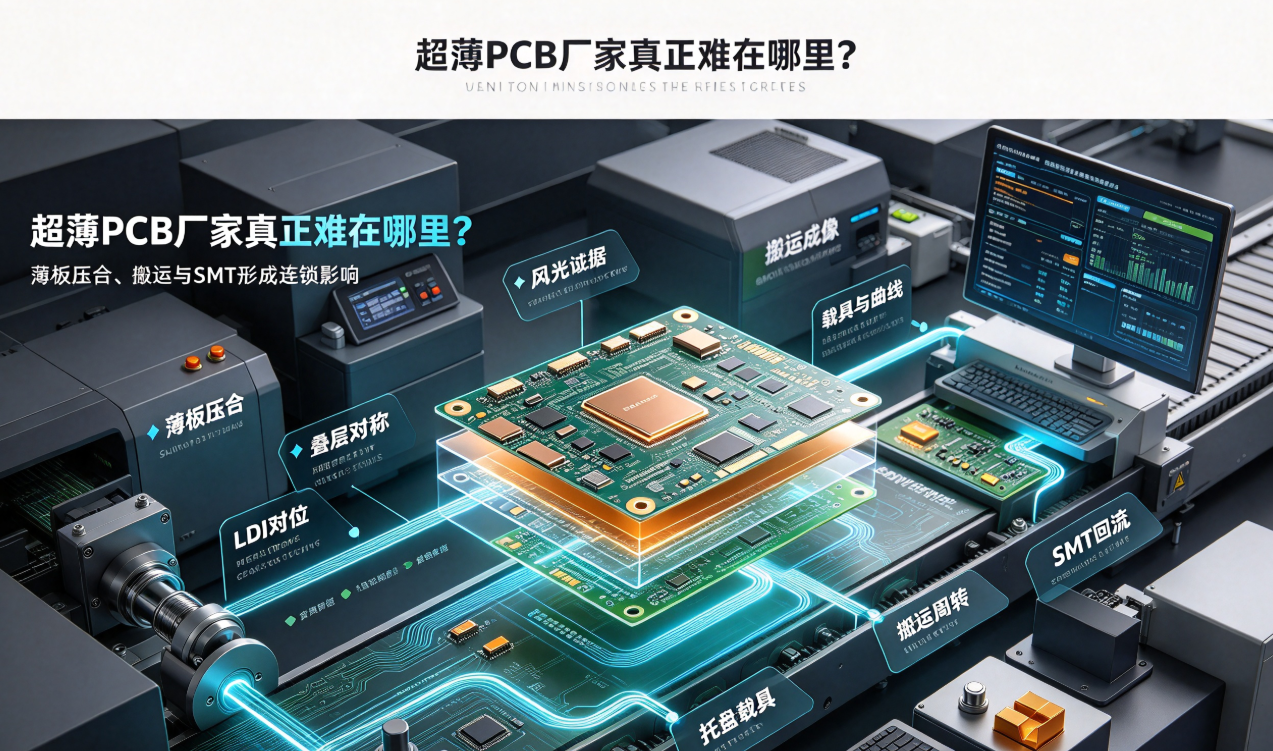
Achieving target thickness in ultra-thin PCBs is only the first step; mass production demands solutions for lamination warpage, pattern misalignment, handling damage, solder paste printing, and reflow support. This article breaks down how thin-board challenges cascade across the manufacturing flow—and what capabilities customers should verify when selecting an ultra-thin PCB supplier.
Producing one ultra-thin PCB is fundamentally different from consistently producing a stable, high-yield batch.
While prototype ultra-thin PCBs can achieve target thickness via manual selection, physical support, and iterative adjustments, volume production requires consistent flatness, dimensional accuracy, trace fidelity, and assembly reliability. As substrate rigidity decreases, copper distribution and lamination behavior propagate issues into imaging, routing, handling, and SMT—creating a cascading effect.
Lamination: Warpage Risk Begins at Stack-Up
Asymmetric materials, copper thickness, or pattern distribution cause differential expansion and contraction during heating and cooling. Ultra-thin PCB suppliers must review stack-up design, copper fill patterns, and large copper-free areas during engineering evaluation; use thin-board-specific supports and lamination formulations; and measure full-panel thickness—not spot measurements.
Imaging & Drilling: Flatness Directly Impacts Registration
Thin substrates are prone to flexure during exposure, etching, and drilling—degrading registration accuracy and annular ring integrity. Laser direct imaging (LDI) improves patterning precision, but still requires dedicated vacuum chucks and handling systems. Minimum line width/spacing, mechanical holes, and laser blind vias must be evaluated against actual 0.15 mm or 0.2 mm stack-ups—not conventional board limits.
Handling: Many Defects Originate Outside Equipment
Manual handling—including picking, stacking, and transfer—can introduce creases, edge damage, and localized contamination, all of which amplify during reflow. Factories must define designated handling zones, deploy trays, isolation materials, and thin-board carriers, and strictly control inter-process dwell time and stacking methods.
SMT: Stencil Printing, Placement, and Reflow Jointly Test Flatness
Board flexure compromises stencil contact and solder paste transfer efficiency; thermal stress during reflow may further exacerbate warpage. Carriers must support critical board areas while avoiding component interference; reflow profiles must be tuned to match board thickness, material properties, and component thermal mass. Acceptance criteria must include pre- and post-reflow flatness, dimensional stability, solder joint quality, and electrical performance.
What Evidence to Review When Selecting a Supplier
- Actual stack-up configurations and volume production records for 0.15 mm and 0.2 mm products.
- Thin-board carriers and process parameters used across lamination, handling, and SMT.
- Pre- and post-reflow flatness, dimensional, and yield data.
- Engineering evaluation capability for high-Tg materials, fine-line circuits, and HDI structures.
Hongyi Precision provides engineering evaluation, prototyping, and volume production for 0.15 mm / 0.2 mm ultra-thin FR4 PCBs. True thin-board capability is proven by end-to-end manufacturing stability—not by the thickness of a single sample.