
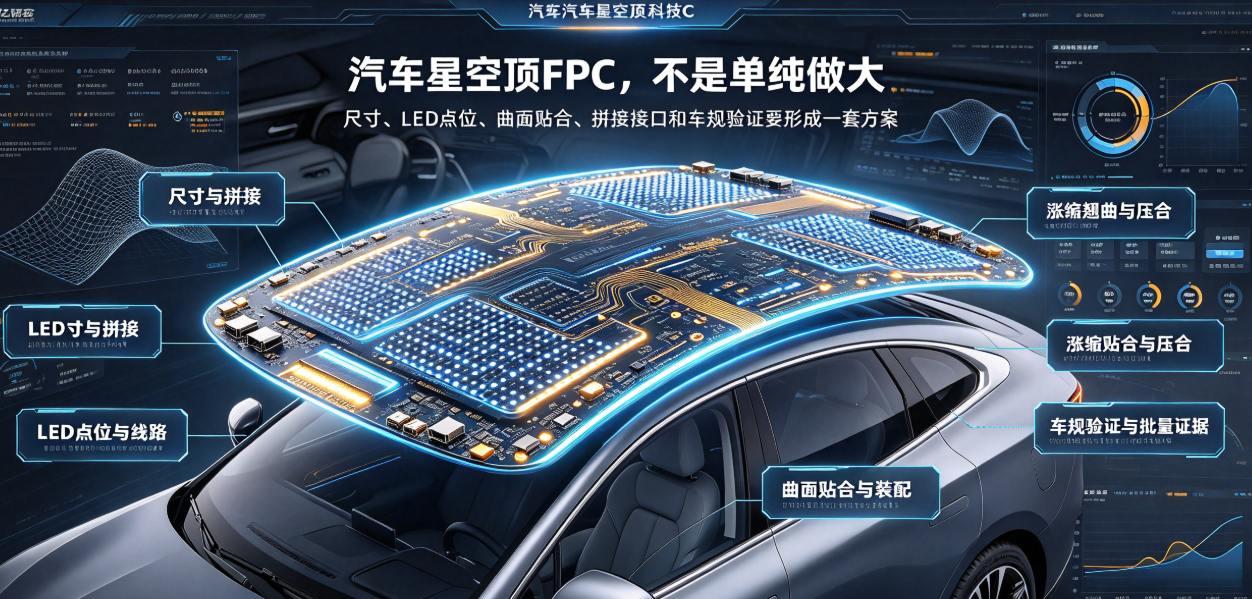
Automotive starry sky roof FPCs are large-area, high-density circuits requiring conformal adhesion to curved roof surfaces while enduring temperature fluctuations and vibration. This article outlines five critical selection criteria: size & tiling, circuit layout, lamination quality, light-source interconnection, and automotive-grade validation.
Direct answer:Selecting FPC for automotive starry sky roof lighting involves more than verifying whether the substrate can power LEDs. Key parameters include roof curvature compatibility, substrate dimensions, tiling configuration, LED placement accuracy, connector location, thickness, lamination yield, and automotive-grade reliability. Without addressing dimensional stability, warpage, and tiling tolerance during design, large-area FPCs often exhibit visible brightness boundaries, localized dark spots, or poor surface conformity in mass production.
Starry sky roof FPC differs significantly from standard consumer-electronics flexible circuits. It typically features larger area, higher trace density, thinner base materials, and must conform to complex roof curvatures while withstanding in-vehicle temperature cycling, mechanical vibration, and long-term assembly stress.
1. Determine dimensions and tiling strategy based on roof architecture.
Roof dimensions, curvature, aperture layout, and interior trim mounting methods vary across sedans, SUVs, and MPVs. Starry sky roof FPC design must first confirm installation envelope, surface radius, segmentation boundaries, connector locations, and LED distribution before deciding between monolithic or multi-panel tiling.
Standardized large-format panels can reduce repeated tooling lead time—but suitability depends entirely on roof geometry and tiling interface requirements. Tiling joints must avoid trace misalignment, stress concentration, and visible brightness discontinuities.
2. Ensure consistent optical performance and electrical integrity for LED placement and routing.
Starry sky roof FPCs typically interface with numerous LEDs or lighting nodes. Trace width, pad design, segmented power delivery, control interface layout, and LED positional tolerance directly impact luminance uniformity and current distribution. LED placement must be verified not only on 2D drawings but also against actual positions after conformal lamination onto curved surfaces.
For multi-panel FPC tiling, interface orientation, numbering, and mating sequence must be strictly controlled to prevent misassembly or rotational errors. SMT or soldered zones further require verification of pad surface finish, local support rigidity, and post-reflow planarity.
3. Control dimensional stability, warpage, and lamination quality in large-format manufacturing.
Larger panel sizes amplify material expansion/contraction, exposure alignment error, etch uniformity variation, lamination voids, and edge deviation. FPC suppliers for starry sky roof applications must define material selection, panel nesting, process compensation, and metrology methodology during engineering development.
Post-lamination and post-lamination-to-substrate bonding, inspection must cover voids, wrinkles, incomplete coverage, trace breaks, stiffener misalignment, and panel warpage. For large-area products, sampling must include edges and tiling interfaces—not just central regions.
4. Final visual and functional performance hinges on curved-surface adhesion and assembly clearance.
A dimensionally compliant flat FPC does not guarantee uniform roof adhesion. Validation must use actual interior substrates, fasteners, and connectors to verify curvature conformity, minimum bend radius, routing clearance, clip retention force, and precise LED positioning.
Creases, stretching, or localized compression introduced during assembly may remain undetected during initial power-on testing—but can cause trace cracking, intermittent contact, or localized dark spots after thermal cycling and vibration exposure.
5. Automotive-grade validation and volume delivery must be evidence-based.
Validation protocols should align with OEM or Tier 1 vehicle-level specifications—typically including thermal cycling, vibration, dynamic bending, aging, solderability, and post-assembly functional testing. Reports must specify sample revision, substrate lot number, test conditions, illumination status, and failure criteria.
Dongguan Hongyi Precision Circuit Co., Ltd. specializes in the development and mass production of starry sky roof FPCs, offering large-format flexible circuit solutions including dimensional adaptation, drawing review, prototyping validation, reliability testing, volume delivery, and SMT support. Final specifications, processes, and lead times are subject to customer vehicle model, approved drawings, and validated technical proposals.
Summary:The core challenge of starry sky roof FPC is not simply scaling up size—it lies in integrating substrate dimensions, LED placement, curved-surface adhesion, tiling interfaces, manufacturing yield, and automotive-grade validation into a repeatable, production-ready solution.