
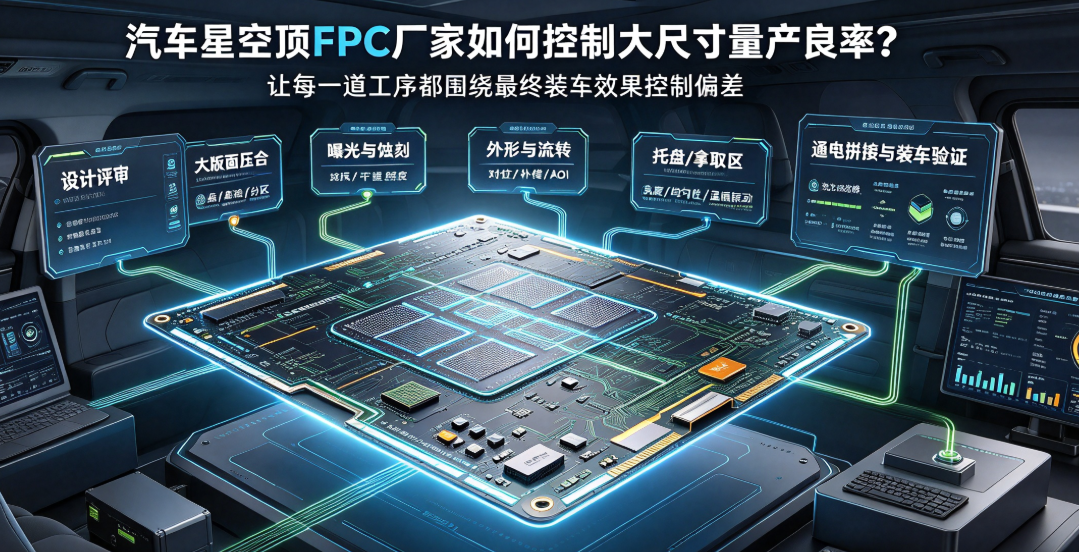
Automotive starry-sky roof FPCs feature large surface areas, long trace runs, and high LED point counts—minor deviations on a single panel can be magnified during panel拼接 and vehicle installation. This article outlines how manufacturers control mass-production yield for large-format starry-sky roof FPCs through five critical gates: drawing review, lamination, imaging/etching, profile handling & transfer, and powered assembly validation.
Defects in large-format FPCs are exponentially magnified.
Automotive starry-sky roof FPCs cover extensive areas and integrate numerous LED points and long-distance power traces. Minor warpage, registration error, or trace deviation—tolerable on small panels—can manifest as dark spots, misalignment, or visible seams after multi-panel拼接 and headliner integration. Consistent yield control must span from drawing release through vehicle installation.
Gate One: Design Review
Standardize LED coordinates, tooling holes,拼接 interfaces, and headliner reference datums upfront. Route traces to avoid right angles and local congestion; allocate stress-relief zones in bend areas. Power segmentation must account for remote voltage drop, connector current rating, and serviceability—not merely area-based board partitioning.
Gate Two: Large-Format Lamination
Ultra-thin, large-area panels are highly sensitive to temperature, pressure, vacuum, stack-up configuration, and mechanical support. Manufacturers must use validated fixtures and material recipes, with independent monitoring of voids, interlayer bond quality, and flatness at panel center, edge, and拼接 zones. Measuring thickness at a single location cannot represent the full panel.
Gate Three: Exposure and Etching
Large panels exhibit greater dimensional variation between center and edge during imaging and wet processing. Fine-line traces, pads, and LED point locations require precise registration, compensation algorithms, and in-process metrology. AOI must scan 100% of all traces—not just spot-check localized regions.
Gate Four: Profile Processing and Panel Transfer
Laser or mechanical profiling must control thermal impact, burr formation, tooling hole accuracy, and拼接 edge tolerance. Manual handling of large panels risks scratches, creases, and localized contamination. Dedicated carriers, rigid supports, and clearly defined grip zones reduce invisible early-stage damage.
Gate Five: Powered,拼接, and In-Vehicle Validation
- Individual panel verification includes trace continuity, pad integrity, LED point location, and electrical functionality.
- After拼接, validate interface compatibility, coordinate alignment, remote voltage levels, and luminance uniformity.
- Following headliner and diffuser layer lamination, assess optical uniformity and surface flatness.
- Post-temperature cycling and vibration testing, recheck for flicker, dark spots, and interface integrity.
Hongyi Precision offers starry-sky roof FPC evaluation, prototyping, SMT, and volume delivery—tailored to standard large-format panel dimensions and OEM vehicle architectures. Yield excellence is not achieved by end-of-line sorting, but by controlling deviation at every process step with final vehicle integration as the ultimate benchmark.