
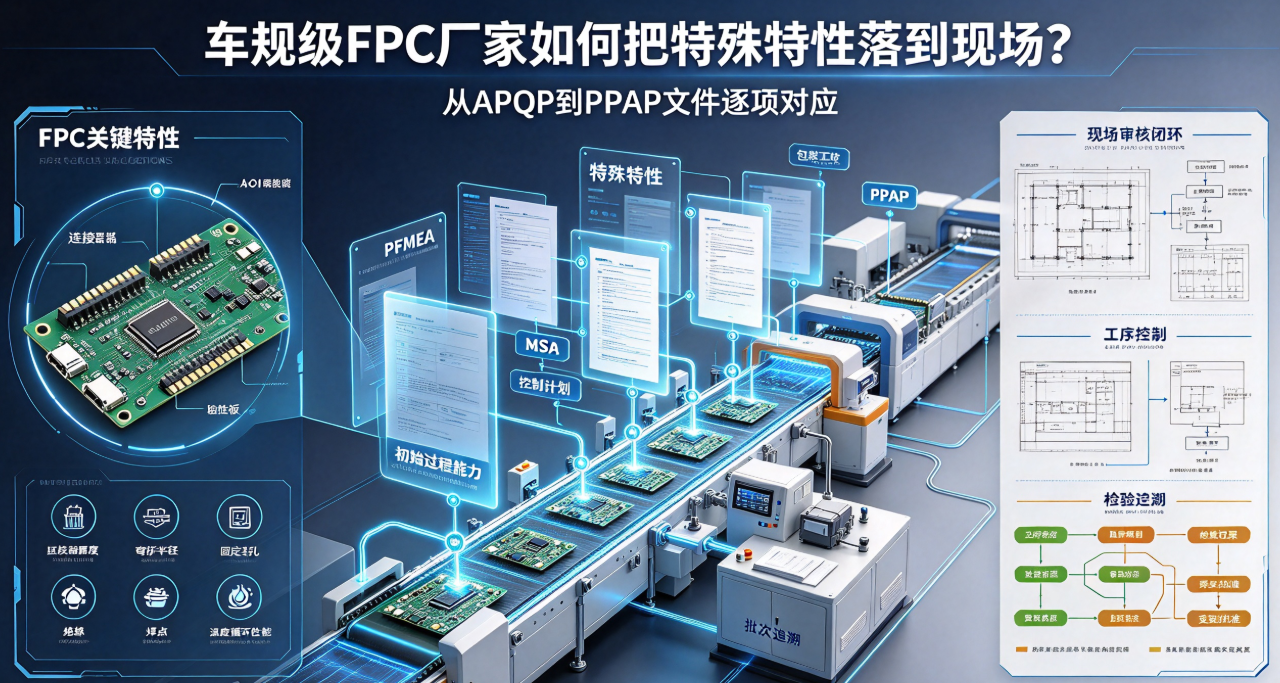
The challenge of automotive-grade FPC projects lies not in producing voluminous documentation, but in ensuring traceable alignment among drawing special characteristics, PFMEA, control plans, inspection records, and PPAP submission items. This article outlines—through the lens of customer audit—the linkage between automotive FPC quality documentation and shop-floor controls.
During customer audits of automotive-grade FPC manufacturers, common questions focus not on whether documentation exists, but on whether documents interlink consistently. If critical dimensions marked on drawings do not appear in the PFMEA or control plan—and are absent from shop-floor inspection records—even comprehensive documentation fails to demonstrate process control.
First, translate the customer’s special characteristics into FPC-specific terminology.
Key characteristics in automotive applications may originate from functional requirements, regulatory mandates, assembly constraints, or safety risks. For FPCs, these may correspond to connector-end thickness, impedance, bend radius, mounting holes, insulation integrity, electrical testing, solder joint reliability, or post-temperature-cycle performance. Engineering teams must articulate why each characteristic matters and the consequences of its failure.
PFMEA must identify specific failure modes.
"Circuit defect" is too generic. More effective analysis distinguishes failure modes such as etching notches, lamination voids, coverlay cracking, stiffener delamination, solder joint fatigue, connector contact instability, and mechanical stress during assembly—and identifies the associated process step, current prevention methods, and detection approach.
The control plan must specify who measures, when, and how.
Each special characteristic must be linked to measurement method, equipment, frequency, sample size, acceptance criteria, record location, and response protocol for nonconformance. For 100% electrical testing, AOI, or critical dimension sampling, equipment capability and re-evaluation rules must be defined—vague statements like "inspect per standard" are insufficient.
Process capability must rest on reliable measurement.
Before calculating capability indices, confirm consistency across gages, fixtures, procedures, and operators. Dimensional stability of flexible circuits, ambient temperature/humidity, and fixturing methods all influence measurement outcomes. Automotive-grade FPC manufacturers should clarify which characteristics suit trend monitoring, which require 100% inspection, and which demand dedicated gaging.
PPAP submission items must be tied to physical parts and lot numbers:
Design records, bill of materials, and engineering change status;
Correspondence among process flow diagrams, PFMEA, and control plans;
Dimensional, material, performance, and reliability validation reports;
Initial process capability, MSA, and trial production yield data;
Production samples, packaging, labeling, and customer-required approval records.
PPAP approval is not the endpoint—documentation requires ongoing maintenance. Changes to materials, equipment, suppliers, production location, process parameters, or inspection methods must be reassessed per impact severity; submission updates and customer re-approval may be required.
Customer auditors may ask three on-site questions:
At which production step is each key characteristic on the drawing controlled?
Can the most recent nonconformance be traced from the shipped lot back to material and process records?
When a material or equipment change occurs, who assesses its impact—and who authorizes implementation?
Hongyi Precision leverages its IATF 16949 quality management system to support automotive FPC projects across engineering review, sample validation, process control, and production documentation. The value of automotive capability lies not in complex documentation—but in enabling every critical risk to be prevented, detected, and traced on the shop floor.