
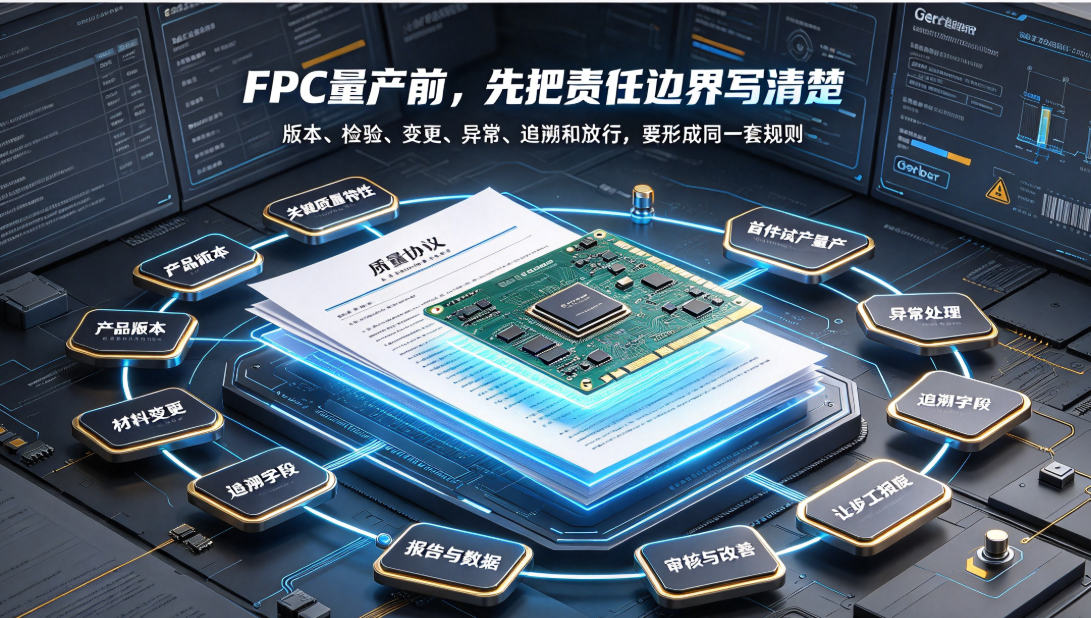
An FPC manufacturer’s quality agreement must go beyond stating 'conforms to drawings.' This article outlines nine critical responsibility boundaries—version control, critical-to-quality (CTQ) characteristics, material changes, release criteria, anomaly handling, traceability, reporting, concession acceptance, and audits—that must be clarified before mass production.
Bottom line first:Before selecting an FPC manufacturer for sampling or mass production—beyond confirming pricing, lead time, and sample results—both parties must clearly define responsibility boundaries in the quality agreement. Without unified definitions for materials, drawings, inspection, changes, anomalies, traceability, release, and claims, projects may appear smooth initially but later face disputes during mass production over 'who is responsible, against which standard, and what is the impact.'
A quality agreement is not merely a document used during audits. It should enable engineering, manufacturing, quality, procurement, and customers to operate under the same version control and judgment rules. For automotive electronics, electronic shifters, and robotics FPC projects, the agreement must also cover application-specific conditions such as flexing, vibration, temperature, and assembly requirements.
1. Clearly specify approved versions of products and supporting documents
The agreement must explicitly state part numbers, drawing revisions, BOMs, stack-ups, materials, surface finishes, stiffeners, connectors, and software or test program versions. When the customer issues updated drawings, the agreement must assign responsibility for assessing change impact—and define how work-in-process and inventory using prior versions will be handled.
If multiple configurations exist under the same part number—e.g., varying thicknesses, stiffener types, or connectors—distinct version or configuration identifiers must be used. Relying solely on verbal notifications or date-based file names invites on-site document misapplication.
2. List critical-to-quality (CTQ) characteristics as measurable items
The agreement must not simply state 'conforms to drawings and industry standards.' Instead, it must identify CTQ characteristics that directly affect functionality and assembly—such as line width/spacing, hole placement, coverlay window dimensions, connector-end thickness, stiffener location, impedance, continuity, insulation resistance, and dimensional tolerances.
For each item, the agreement must specify measurement reference points, methods, equipment, frequency, sampling size, and acceptance criteria. Measurement condition is especially critical for flexible circuits: results may differ significantly between free-state, fixture-mounted, and assembled-state measurements.
3. Material and supplier changes require advance communication
Changes to polyimide (PI), copper foil, adhesive systems, coverlay, stiffeners, surface finishes, or connectors may affect thickness, flex life, solderability, thermal resistance, and dimensional stability. The quality agreement must differentiate between general substitutions, critical material substitutions, and emergency shortage responses—and define notification, evaluation, sampling, revalidation, and approval procedures.
Unapproved material substitutions must not proceed to mass production—even if electrical performance tests pass on samples. The agreement must also clarify which work-in-process, inventory, and shipped batches are impacted by any material change.
4. Release criteria must be differentiated for first-article, pilot-run, and mass production
Engineering samples aim to validate design and assembly; small-batch pilot runs verify process repeatability; and mass production release confirms batch consistency, yield, inspection status, and delivery readiness. These three stages must not be conflated under a single 'approved' conclusion.
The agreement may separately define submission requirements for first-article reports, reliability test reports, process capability data, outgoing inspection records, and customer approvals. It must specify which items must be completed before shipment—and which permit only sample delivery.
5. Anomaly response must define timelines and required information
Upon detecting opens, shorts, intermittent faults, pad defects, stiffener misalignment, or assembly interference, the manufacturer must first isolate affected lots, then assess scope. The agreement must stipulate notification deadlines, interim containment actions, impacted lot identification, preliminary root cause analysis, rework methodology, and reinspection requirements.
"Issue resolved" or "enhanced inspection" does not constitute a complete anomaly resolution. Customers require clarity on: which units were isolated, which have already shipped, how impact scope was determined, from which lot corrective actions take effect, and how recurrence prevention is verified.
6. Traceability fields must enable actual root-cause identification
Traceability is more than recording a shipment date. At minimum, fields must link—per project requirements—material lot numbers, production work orders, drawing revisions, key equipment or processes, inspection results, rework records, packaging labels, and shipment batches.
For automotive and robotics projects, traceability must also support sample retention, correlation of reliability test samples, and rapid isolation of nonconforming lots. Insufficient traceability fields force broad production stoppages during issues; well-defined fields narrow impact scope effectively.
7. Scope of inspection reports and raw data submission must be explicit
The agreement must distinguish between routine outgoing reports, periodic customer reports, anomaly analysis packages, and audit support documents. Whether dimensional, electrical, material, reliability, or process records require raw data—and their retention duration and submission format—must be pre-agreed.
Generic system certifications (e.g., ISO 9001, IATF 16949) cannot substitute for batch-specific inspection results. For CTQ characteristics, customers may require reports to include part number, revision, batch ID, sample size, equipment used, and acceptance criteria—to prevent historical data from being misapplied to new batches.
8. Concession acceptance, rework, and scrap require defined approval authority
When products deviate from specifications yet remain potentially fit for use, the agreement must specify whether concession acceptance is permitted, who holds approval authority, and whether quantity limits or usage restrictions apply. Unauthorized sorting, rework, or split shipments must not replace formal quality decisions.
Reworked units must undergo clearly defined reinspection. Scrap and nonconforming items require documented isolation and disposition. Concession batches must be fully traceable to order, quantity, and customer approval—to prevent inadvertent mixing with conforming lots.
9. Audits, changes, and continuous improvement must form a closed loop
During customer audits of FPC manufacturers, focus should center on project-specific evidence—including drawing control, material storage, in-process inspection, anomaly handling, and traceability—not generic marketing materials. The agreement must also define audit notification timelines, corrective action deadlines, verification methods, and escalation protocols for recurring issues.
When quality data reveals recurring defect patterns, the manufacturer must embed improvements into drawings, process parameters, work instructions, inspection standards, and training—not merely perform sorting on individual lots. Improvement effectiveness must be confirmed via subsequent production lots or validation samples.
FPC Manufacturer Quality Agreement Checklist
Part numbers, drawing revisions, BOMs, materials, and test program versions;
CTQ items, measurement references, methods, frequencies, and acceptance criteria;
Notification and approval procedures for material, subcontractor, equipment, and process changes;
Release criteria for first-article, pilot-run, mass production, and reliability validation;
Anomaly notification, containment, impact scope, corrective actions, and response timelines;
Traceability linking materials, work orders, inspections, rework, packaging, and shipment batches;
Reporting scope, raw data requirements, sample retention, and document retention periods;
Authority for concession acceptance, rework, scrap, and nonconforming item disposition;
Closed-loop mechanisms for audits, corrective actions, revalidation, and continuous improvement.
Why the quality agreement reflects an FPC manufacturer’s professionalism
A professional FPC manufacturer does not reduce quality responsibility to 'manufacturing per customer drawings.' Instead, it proactively confirms documentation, operating conditions, CTQ characteristics, and validation boundaries at project kickoff—and transforms production risks into jointly executable records and decision rules.
Dongguan Hongyi Precision Circuit Co., Ltd. supports automotive electronics, humanoid robotics, and consumer electronics projects with drawing review, DFM analysis, engineering sampling, in-process inspection, reliability validation, FPCA assembly, and mass production. Specific quality agreement content shall be determined based on customer drawings, quality standards, product structure, and mutually approved documents.
For reference on project documentation confirmation, seeDFM Review Methodology for FPC Manufacturers, for first-article and mass production release, seeKey Evidence for First-Article Confirmation by FPC Manufacturers, and for in-process quality control, seeIn-Process Inspection and Nonconforming Lot Release by FPC Manufacturers.
Summary:The purpose of a quality agreement is to align the customer and FPC manufacturer on a common set of rules governing product versions, inspection methods, anomaly handling, change approvals, and delivery responsibilities. The clearer the boundaries, the faster issues can be located and resolved during mass production—and the stronger the foundation for stable, reliable delivery.