
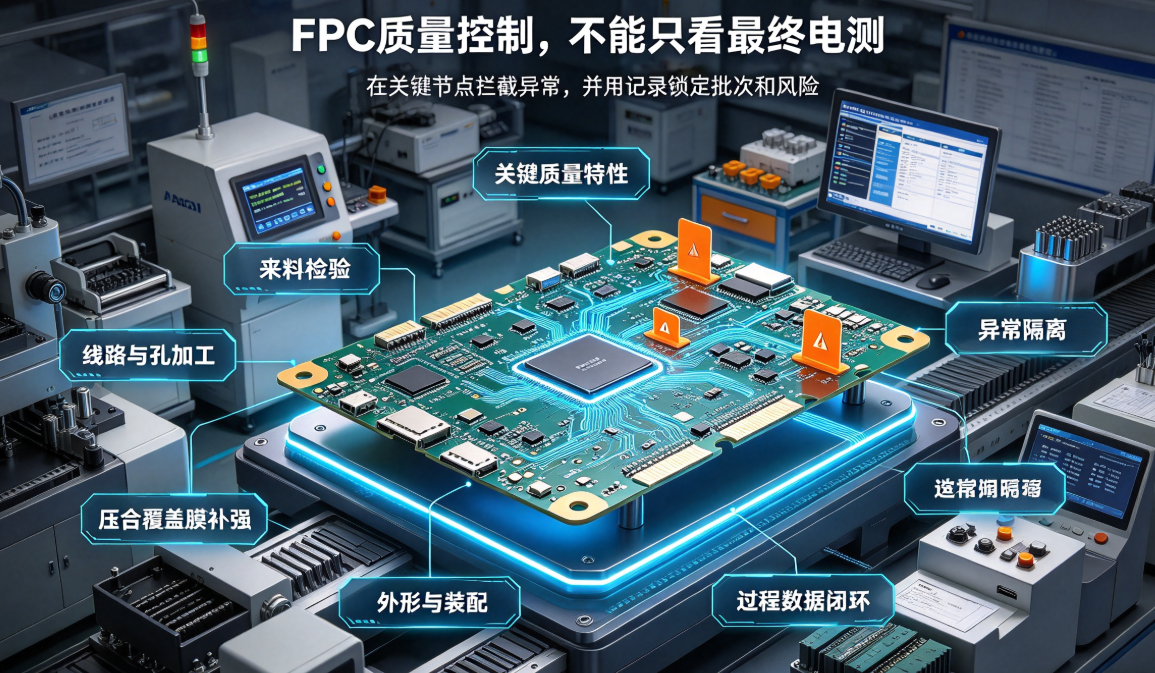
FPC manufacturers must not wait until shipment to perform process inspection. This article outlines quality control methods—from IPQC to batch release—across seven areas: critical quality characteristics, incoming materials, circuitry, lamination, assembly, anomaly isolation, and data closure.
First, the conclusion:Assessing whether an FPC manufacturer possesses stable mass-production capability cannot rely solely on final electrical test pass rates—or wait until shipment inspection to uncover issues. Truly effective quality control requires in-process inspection at critical nodes—including materials, circuitry, lamination, stiffener application, outline formation, and assembly—and ensures timely isolation, evaluation, disposition, and traceability of abnormal batches.
FPCs are flexible structures; many defects remain latent early on and only manifest after lamination, bonding, bending, or assembly. Well-executed process inspection intercepts issues before they escalate into higher-cost operations; poor execution allows defects to propagate through to finished goods—or even to customer assemblies—resulting in rework, delays, and batch-level risk.
1. First, identify critical quality characteristics.
Process inspection does not entail uniform sampling across every operation. Instead, critical quality characteristics must first be identified based on product structure and application conditions. Common items include trace width/spacing, hole location, coverlay window alignment, connector-end thickness, stiffener placement, dimensional tolerances, impedance, continuity, and insulation resistance.
For automotive electronics, electronic shifters, and robotic dynamic FPCs, additional requirements include bend radius, mounting point positioning, motion clearance, pad stress tolerance, and critical functional signal integrity. Each characteristic must be linked to a defined measurement method, reference standard, inspection frequency, and acceptance criterion—otherwise, inspection records cannot support release decisions or traceability.
2. Incoming material inspection determines downstream stability.
The type, thickness, lot number, and storage condition of PI, copper foil, coverlay, adhesive film, stiffeners, and surface finishes directly impact dimensional stability, bend performance, solderability, and thermal resistance. Incoming inspection must go beyond label verification and confirm material conformity against approved BOMs and stack-up specifications.
When material substitutions, lot mixing, expired shelf life, or visible damage are detected, affected materials must be isolated immediately and fully evaluated. Once nonconforming materials enter lamination or bonding, subsequent final electrical testing often fails to detect resulting defects.
3. Circuit and hole processing must be intercepted at intermediate stages.
Exposure, developing, etching, drilling, and via metallization directly affect traces, pads, and interlayer connections. IPQC should integrate AOI, trace width/spacing, hole location, hole diameter, hole wall quality, and copper thickness measurements—with special attention to board edges, high-density routing areas, narrow necks, and regions with dense via placement.
If residual copper, notches, registration misalignment, or abnormal via plating are observed, simply removing one defective unit is insufficient. The root origin—including time frame, involved materials, and work-in-process lots—must be determined, and related batches isolated accordingly.
4. Lamination, coverlay, and stiffener application must verify structural outcomes.
After lamination and coverlay lamination, inspections must cover voids, wrinkles, resin bleed, window misalignment, incomplete coverage, and foreign particles. For stiffener areas, focus must extend to placement accuracy, planarity, total thickness, and transition zone smoothness—especially near connector ends and dynamic bend initiation points.
Such defects may not immediately cause open circuits but can alter local rigidity, solder joint integrity, or assembly clearance. Process inspection must go beyond visual photography—employing dimensional measurement, thickness gauging, peel testing, or functional assembly verification to confirm functional impact.
5. Outline forming and assembly must be inspected against defined references.
After die-cutting, punching, laser cutting, or CNC machining, checks must cover overall length/width, hole locations, branch geometry, narrow neck dimensions, and connector-end features. Flexible substrates deform easily in free state; measurements must follow customer drawing-specified datums, fixtures, and physical states—not arbitrary straightening followed by recording of deceptively ‘clean’ dimensions.
For FPCA or connector-integrated products, additional checks include insertion force, locking engagement, solder joint integrity, component height, housing clearance, and motion trajectory validation. A dimensionally compliant bare board that interferes during assembly indicates process inspection failed to reflect actual usage conditions.
6. Abnormal batches must be isolated before release decisions.
Upon detecting anomalies during process inspection, the first step is identification and isolation of affected raw materials, work-in-process, and finished goods. Only then should disposition options—rework, scrap, sorting, or concession—be evaluated. The scope of impact must be defined using time stamps, equipment IDs, material lots, work orders, and inspection results—not limited to the single sampled unit.
If rework or sorting is applied, revised inspection criteria and retest quantities must be formally established. Concession releases require formal approval from the customer or authorized quality representative, accompanied by documented risk acknowledgment. ‘Ship-first, document-later’ practices without prior approval compromise batch status control.
7. Process data must link back to root causes and improvements.
Effective IPQC records capture more than pass/fail status—they log equipment ID, process parameters, operator, material lot, inspection timestamp, defect type, and disposition outcome. When recurring notches, misalignments, or voids appear at identical locations, such data enables engineering teams to determine whether root causes lie in materials, equipment, process window limits, or operator conditions.
After corrective actions are implemented, verify that control plans, work instructions, inspection standards, and training records have been updated accordingly—and validate effectiveness using subsequent production batches. Merely noting ‘enhanced controls’ in an exception report—without updating process documents—typically fails to prevent recurrence.
FPC Manufacturer Process Inspection Checklist:
Drawing, BOM, material, process, and inspection document versions are aligned;
Incoming material type, thickness, lot, storage condition, and substitution status are controlled;
Intermediate inspections exist for circuitry, hole location, via plating, coverlay, stiffeners, and outline;
Specialized checks cover connector ends, solder joints, assembly clearances, and dynamic zones;
Nonconforming materials and work-in-process carry clear identification, isolation, and impact assessment;
Rework, sorting, concession release, and reinspection are approved and documented;
Process data links to equipment, material lots, defect types, and improvement outcomes.
What distinguishes process inspection from final inspection?
Final inspection answers: ‘Do these finished goods currently meet release criteria?’ Process inspection answers: ‘When did this issue arise during manufacturing? Which products may be affected? And how can risk be contained before further resources are invested?’ These two functions are not interchangeable.
For FPC manufacturers, final electrical test pass rate remains important—but it cannot replace material traceability, circuit AOI, dimensional checks, coverlay integrity, stiffener verification, assembly validation, or reliability testing. Only when process and finished-goods data mutually corroborate can customers confidently assess supplier mass-production stability.
How Hongyi Precision Supports Mass-Production Quality Control
Dongguan Hongyi Precision Circuit Co., Ltd. provides drawing review, DFM analysis, engineering prototypes, process inspection, assembly verification, reliability validation, FPCA integration, and volume production support for automotive electronics, humanoid robotics, and consumer electronics programs. Full capability details are available atFPC Manufacturer and Flexible Circuit Board Manufacturing Services, and manufacturing workflow is outlined inFPC Manufacturer Production Flow and Critical Processes.
Prior to mass production, joint confirmation perFPC Manufacturer First-Article Approval and Mass-Production Release Evidenceis required to lock down version control, critical quality characteristics, and approved boundaries. Specific inspection items, sampling plans, anomaly handling procedures, and release criteria shall follow customer drawings, quality agreements, and mutually approved documents.
Summary:The value of FPC process inspection lies not in adding more forms—but in identifying issues before defects proliferate, isolating associated risks, and generating traceable evidence. Closing the loop among IPQC execution, anomaly disposition, and mass-production control forms the foundation of reliable FPC manufacturer delivery.