
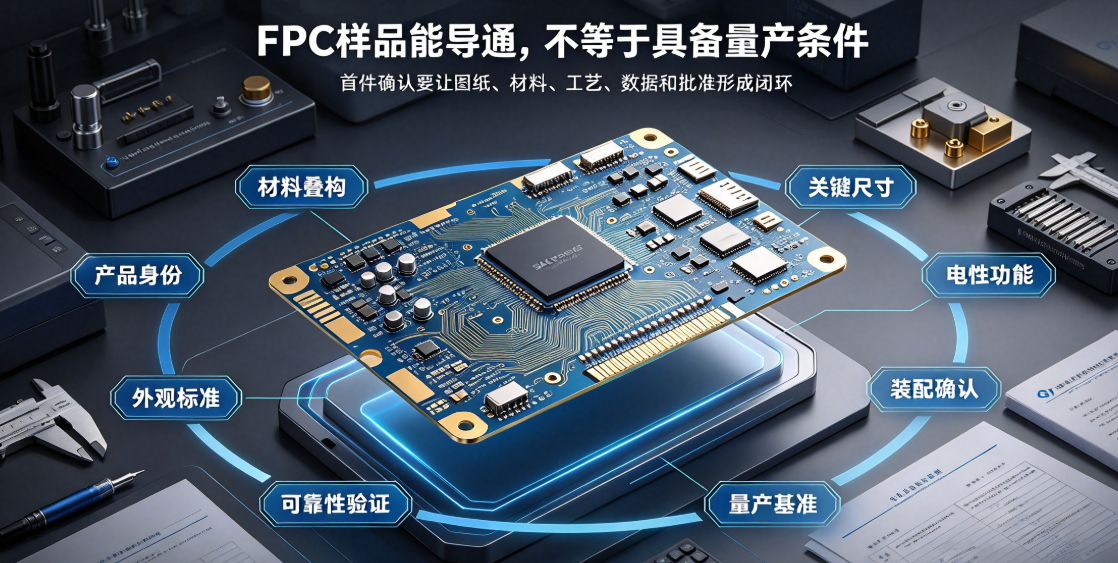
First-article approval for FPC manufacturers must go beyond continuity testing. This article outlines eight critical verification areas—version control, materials, dimensions, electrical performance, appearance, assembly, reliability, and production control—that must be confirmed before flexible circuit boards enter mass production.
To state the conclusion upfront:An FPC sample passing continuity testing does not mean it is ready for mass production. The purpose of first-article approval is to demonstrate, prior to volume manufacturing, that 'this drawing revision, these approved materials, this process route, and this inspection methodology' can consistently produce parts meeting all requirements. A professional FPC manufacturer does not simply provide a photo of a passing sample; instead, it correlates dimensional, electrical, visual, assembly, material, and validation results to specific revisions and lot numbers.
Many mass-production issues stem not from final inspection, but from unclear or incomplete requirements during first-article review: unmarked dynamic bend zones, connector-end thickness not controlled separately, coverlay window datums not confirmed, or samples temporarily reworked and mistakenly treated as representative of standard process output. The more comprehensive the first-article review, the fewer engineering changes, rework cycles, and batch-level disputes occur later.
1. Confirm which product revision the first article represents
The first item in a first-article report is not dimensional measurement—it is identity verification. Part number, drawing revision, engineering change notice (ECN), BOM, stack-up, material grade, surface finish, stiffener configuration, and customer purchase order must all align. If one part number has multiple variants—e.g., different connectors, stiffeners, or bend requirements—a single generic report is insufficient.
Sample labels must retain production lot, material lot, and inspection date. When drawings change after first-article completion, it must be explicitly stated which items require remanufacturing, remeasurement, or revalidation.
2. Verify materials and stack-up match approved status
Polyimide (PI), copper foil, adhesive system, coverlay, stiffeners, and surface finishes directly impact thickness, flex life, solderability, dimensional stability, and thermal resistance. First-article confirmation must go beyond stating 'materials compliant'—it requires verification of material grade, thickness, lot number, and stack-up relationships.
If materials were substituted temporarily to meet schedule, the substitution rationale, impact assessment, and customer approval status must be documented. Unassessed alternative materials must not proceed to mass production—even if electrical test results are acceptable.
3. Measure critical dimensions relative to assembly datums
Overall length and width are only baseline dimensions. For electronic shifters, automotive modules, and robotic FPCs, special attention must be paid to connector-end thickness, contact pad location, stiffener boundaries, mounting holes, outline branches, coverlay windows, and bend initiation points. Measurement datums must match those specified on the customer drawing.
Flexible circuits deform easily in free state; dimensions must not be measured after forcibly straightening or flattening the board. For features involving mechanical fit, certified gauges or functional mock-ups should be used to verify insertion, latching, clearance, and motion envelope.
4. Electrical testing must cover critical nets and functionality
Final electrical testing typically detects opens, shorts, continuity, and insulation failures—but first-article review must also confirm alignment of test program, netlist, fixture design, and pass/fail thresholds with the current revision. Products requiring impedance control, high-speed signaling, shielding, or current-carrying capacity cannot rely solely on basic continuity results for release.
If the FPC is assembled with connectors or active components, first-article review must include mating/unmating force, latch integrity, solder joint quality, functional signal integrity, and full-system interface verification. Passing electrical tests but failing post-assembly functionality usually indicates incomplete first-article scope.
5. Visual inspection must follow standardized criteria
First-article review must document line breaks, residual copper, burrs, scratches, creases, coverlay lifting, voids, contamination, stiffener misalignment, and pad condition. Inspection conditions—including lighting, magnification, viewing angle, reference standards, and defect classification—must be defined; 'appearance OK' is not an acceptable conclusion.
High-risk zones—including dynamic bend areas, connector ends, and solder regions—must be photographed separately or clearly annotated in the report. Whether minor visual defects affect function depends on location, size, and actual assembly conditions.
6. Assembly verification must simulate real-world usage
A board may pass flat-state inspection yet fail inside its housing due to clip-induced stress, connector misloading, harness tension, or interference with moving parts. First-article assembly verification should use actual enclosures, connectors, fasteners, and harnesses to validate routing, bend radius, clearance, and extreme positional states.
For electronic shifters or robotic dynamic FPCs, functional monitoring—including continuity, resistance, or signal integrity—must occur during motion. Static assembly alone cannot validate long-term operational reliability.
7. Reliability testing must derive from actual operating conditions
While full-life testing may not be completed at first-article stage, it must be explicitly defined which tests are required for release, which belong to design validation, and which are scheduled for production sampling. Bend cycling, thermal cycling, vibration, damp heat, solderability, and peel strength tests must specify sample revision, quantity, test conditions, fixturing, monitoring method, and failure criteria.
'Test passed' is not a complete conclusion. Both customer and FPC manufacturer must understand what risks the test covers, whether samples reflect current process capability, and whether results support pilot-run and mass-production release.
8. The first-article report must guide subsequent mass production
A qualified first article is not a one-time archival document. The report must record key dimensional data, material lots, process route, equipment or fixtures used, inspection methods, nonconformance disposition, approvers, and effective production lot—establishing the baseline for in-process audits and outgoing inspection.
If first-article issues are identified, manual correction on the sample alone is insufficient. Design issues require drawing updates; material issues demand specification revisions; manufacturing issues necessitate parameter or control plan adjustments; and assembly issues call for structural or work instruction changes—each followed by re-approval.
FPC Manufacturer First-Article Checklist
Part number, drawing revision, BOM, ECN, and PO identification;
PI, copper foil, coverlay, stiffener, surface finish, and material lot;
Overall dimensions, connector-end, stiffener, hole locations, coverlay windows, and bend zones;
Continuity, insulation, impedance, current-carrying capacity, or critical functional testing;
Traces, coverlay, pads, stiffeners, edges, and contamination—visual inspection items;
Actual enclosure, connector, fasteners, clearance, and motion envelope;
Reliability test items, conditions, sample size, acceptance criteria, and report reference;
Nonconformance closure, approval status, mass-production control plan, and lot traceability.
Why first-article approval reflects a true FPC manufacturer’s capability
A general PCB shop may produce a working sample—but a professional FPC manufacturer must explain why the sample passes, which parameters drive the result, how the same outcome will be replicated in the next lot, and how deviations will be assessed for impact scope. The more detailed the first-article documentation, the lower the communication overhead across engineering, quality, manufacturing, and customer teams.
Dongguan Hongyi Precision Circuit Co., Ltd. supports automotive electronics, humanoid robotics, and consumer electronics projects with drawing review, DFM analysis, engineering prototypes, assembly verification, reliability validation, FPCA assembly, and mass-production support. Specific first-article items and release criteria are governed by customer drawings, product structure, quality agreements, and mutually approved documents.
For clarification on phase distinctions between sample acceptance and mass-production release, refer toEngineering Methods for FPC Sample Acceptance and Mass-Production Release; for production process details, refer toFPC Manufacturer Production Flow and Key Process Steps; for overall capability overview, seeFPC Manufacturers and Flexible Circuit Board Manufacturing Services.
Summary:The core of first-article approval is not listing as many inspection items as possible—but ensuring every critical requirement is supported by a corresponding sample, validated method, objective data, and formal approval. Only when first-article evidence becomes actionable process control can an FPC manufacturer truly establish a stable foundation for mass production.