
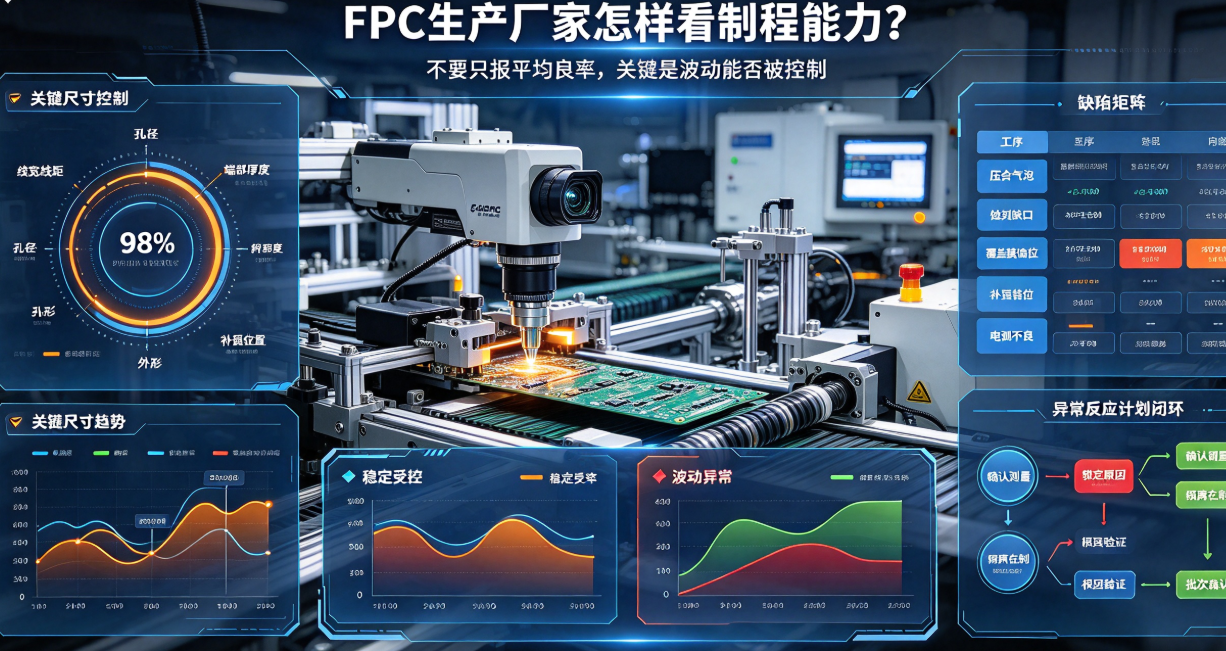
A true assessment of an FPC manufacturer’s capability cannot rely solely on monthly production area or first-run yield. This article outlines how procurement and quality teams can assess process stability by examining critical dimensions, process capability, defect stratification, equipment calibration, and batch trends.
When auditing FPC manufacturers, customers often begin by asking, “What is your monthly capacity and yield?” While these two figures support initial screening, they are insufficient to determine whether a specific FPC design can be delivered consistently. Real production capability ultimately depends on whether critical dimensions remain continuously within specification, whether anomalies are detected promptly, and whether the same process can be replicated across batches.
First, distinguish between capacity, output, and effective capacity
Equipment theoretical capacity does not equal effective output. Line changeovers, material waiting time, fixture occupancy, bottleneck operations, rework, and scrap all reduce deliverable volume. When evaluating a project, FPC manufacturers should calculate capacity based on the customer’s product specifications—including layer count, trace width/space, surface finish, stiffener requirements, and test scope—rather than applying generic plant-wide promotional figures.
Critical dimensions require a validated measurement system
Parameters such as trace width/space, hole diameter, outline dimensions, end thickness, stiffener placement, and connector contact points must be measured using consistent reference standards, equipment, frequency, sample size, and acceptance criteria. If different inspectors apply different methods, even large volumes of data cannot reflect true process variation.
For flexible circuits, measurement condition is especially critical. Results may differ significantly between free-state, flattened-state, and fixture-mounted conditions. Drawings must specify measurement posture and datum to avoid misclassifying assembly issues as purely dimensional defects.
Beyond average yield: examine variation and defect structure
Two manufacturers reporting 98% yield may exhibit vastly different behaviors—one delivering stable 98% across all batches, another delivering several strong batches followed by one with widespread scrap. Customers should require suppliers to break down yield data by process step and defect type, tracking whether lamination voids, etching notches, coverlay misalignment, outline burrs, stiffener misplacement, or electrical test failures cluster around specific equipment, shifts, or material lots.
Process capability is not just a single-number calculation
For critical dimensions, process trend analysis and capability indices (e.g., Cpk) can be applied—but only if the measurement system is reliable and the process is in statistical control. If data includes mixed states—such as pre- and post-material change, equipment maintenance, or process parameter adjustments—a single calculated capability index will mask real risks.
A more practical approach is to establish control charts or trend logs for each critical characteristic, clearly defining warning limits near specification boundaries, stop-line conditions, reinspection scope, and engineering responsibility for process adjustments.
The effectiveness of an anomaly response plan determines whether data is actionable
When a trend shift is observed, first verify the measurement system and sample identity;
Then isolate potential root causes by material, equipment, parameters, personnel, and environment;
Quarantine affected in-process units to prevent further flow of nonconforming batches;
Implement interim containment, validate root cause, and execute permanent corrective actions;
Confirm effectiveness using subsequent batches—not merely by closing an NCR.
What evidence can customers verify on-site?
Consistent batch yield and primary defect trends for products similar to the target part;
Raw measurement records for trace width, hole diameter, outline dimensions, and end thickness;
Calibration and maintenance status of AOI systems, electrical testers, measuring instruments, and key production equipment;
Records of quarantine, traceability, correction, and effectiveness verification for nonconforming batches;
Traceable linkage among material lot numbers, process parameters, and shipped batch IDs.
Hongyi Precision recommends that customers audit FPC manufacturers with the target product in mind—focusing on whether data maps to specific batches, whether anomalies are closed-looped, and whether the process is consistently repeatable. This approach reflects actual delivery capability more accurately than evaluating equipment brands or factory floor area alone.