
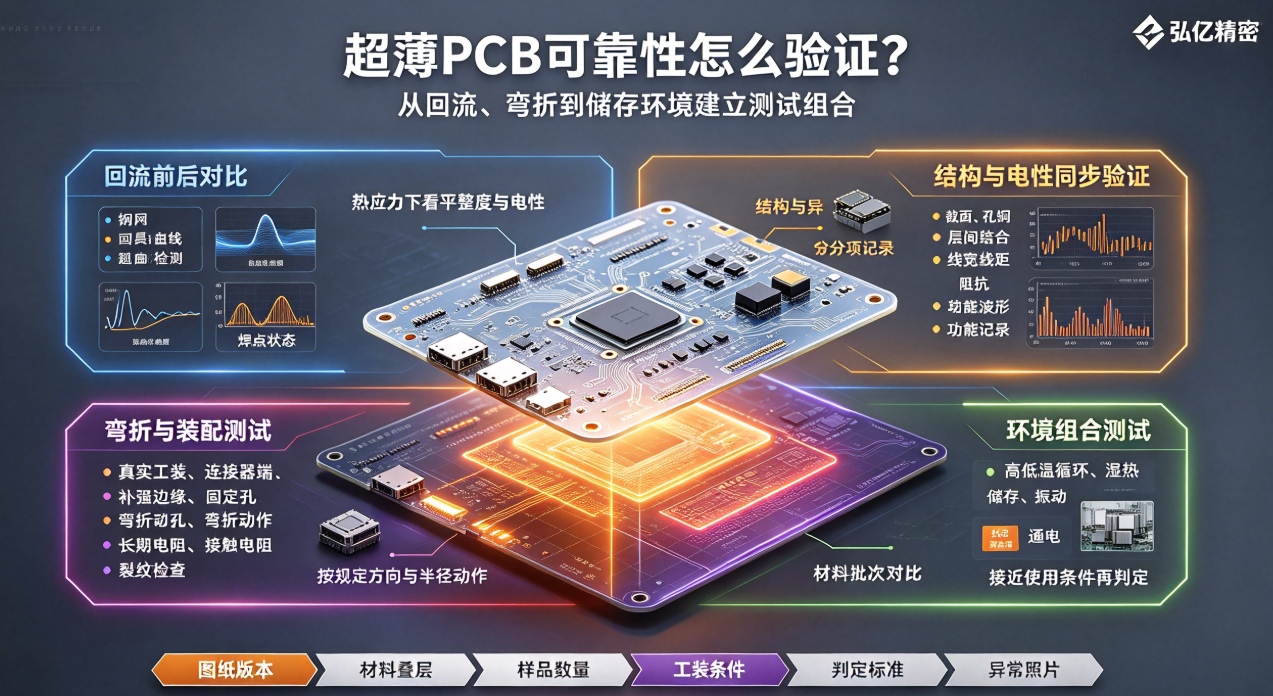
Reliability risks for ultra-thin PCBs are distributed across lamination, handling, SMT, thermal exposure, and storage. This article establishes a test suite based on failure mechanisms—explaining why continuity testing and a single reflow cycle are insufficient to prove thin-board reliability.
Ultra-thin PCB reliability cannot be summarized by 'continuity pass.' As board thickness decreases, warpage, interlayer adhesion, via integrity, solder joint coplanarity, handling-induced flex damage, and dimensional changes under environmental stress all become more sensitive. A sound test plan must originate from failure mechanisms—not simply replicate standard PCB test items.
First, identify key risks for ultra-thin boards
Lamination may introduce voids, delamination, or inconsistent thickness; drilling and copper plating may cause barrel wall or bottom-of-hole defects; SMT may suffer from inadequate stencil contact or reflow-induced warpage; assembly may generate creases or connector mechanical stress; high/low temperature and humidity cycles may exacerbate material shrinkage and insulation degradation.
Compare pre- and post-reflow conditions
Record surface flatness, critical dimensions, pad and component status, then perform actual stencil printing, fixture loading, and reflow. Post-reflow, reinspect warpage, solder joints, component misalignment, impedance, or functional performance. Relying solely on pre-reflow visual inspection and electrical testing fails to capture thermal-stress responses unique to thin substrates.
Structural and electrical validation must proceed in parallel
Multi-layer ultra-thin boards require cross-section analysis, via copper thickness, interlayer bond strength, and dielectric thickness verification; fine-pitch traces demand line width/spacing and insulation checks; high-speed signal designs further require impedance and signal integrity comparison. Structural pass with electrical drift—or electrical pass with localized delamination—must each be recorded as distinct risk events.
Flexing and assembly testing must not be omitted
If the product requires mating, conformal bonding, or localized bending, use production-equivalent or validated tooling to complete assembly, then execute motion per specified direction and bend radius. Connector ends, stiffener edges, and mounting holes are priority zones; inspect for cracks, creases, contact resistance, and functionality before and after testing.
Environmental test combinations must mirror real-world usage
Temperature cycling and dwell at extremes;
Insulation resistance and visual inspection after damp heat exposure, storage, and moisture absorption;
Functional performance under vibration, mating/unmating, or assembly-induced stress;
Flatness after reflow, thermal aging, and extended power-on operation;
Comparative testing across material lots and process revisions.
Test reports must support reproducibility
Reports shall document drawing revision, material and stack-up specifications, board thickness measurement method, sample quantity, fixtures used, temperature profiles, motion parameters, acceptance criteria, and annotated anomaly photos. Reporting only 'pass'—without test conditions and raw data—severely limits traceability and prevents reliable production release decisions.
Hongyi Precision develops tiered test plans for ultra-thin PCBs based on thickness, layer count, signal requirements, SMT configuration, and assembly conditions. Ultra-thin PCB reliability is not determined by a single test—it is demonstrated collectively through manufacturing, assembly, and environmental performance data.