
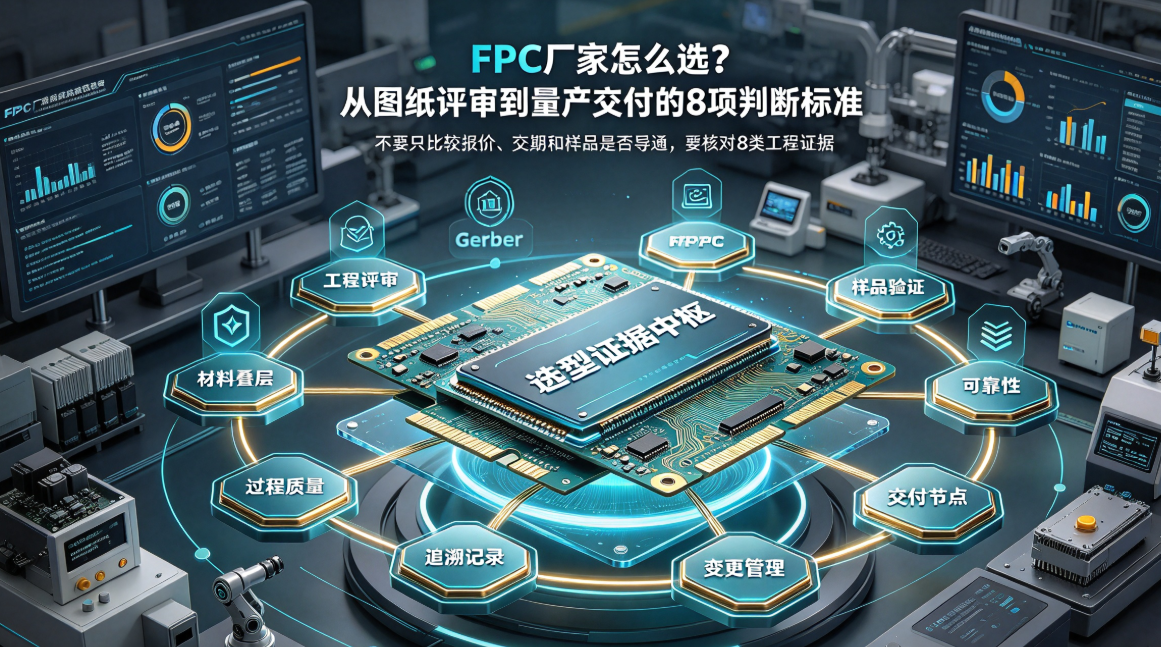
How to select an FPC manufacturer? This article outlines eight evaluation criteria — drawing review, DFM, material stack-up, sample validation, process quality, reliability, delivery, traceability, and change management — for procurement and engineering teams when selecting FPC suppliers.
Direct answer:Selecting an FPC manufacturer should not rely solely on quotation, lead time, equipment count, or whether a single sample passes continuity testing. A more reliable approach is to verify eight categories of evidence — engineering review, material stack-up, sample validation, process quality, reliability, delivery, traceability, and change management — against the same drawing revision and identical application conditions.
From prototype to mass production, FPC project risks rarely stem from a single process step; rather, they arise from misalignment among requirements, mechanical structure, materials, flexing, connectors, inspection, and delivery. A professional FPC manufacturer must identify issues before material release, validate design solutions during sampling, and consistently replicate results in mass production.
1. First, assess whether the manufacturer truly understands your project.
Complete project input includes not only Gerber files but also schematics or netlists, BOMs, stack-up specifications, material types, copper thickness, coverlay, stiffeners, surface finishes, 3D mechanical structures, connectors, mounting points, bend paths, temperature/vibration profiles, current-carrying capacity, and impedance requirements.
Application conditions vary significantly for electronic shifters, automotive FPCs, robotics FPCs, and dexterous-hand FPCs — and so do design priorities. A manufacturer that identifies bending, assembly, signal integrity, or material risks during pre-quotation review demonstrates engineering-level engagement, not just manufacturing quoting.
2. DFM feedback must specify locations and technical rationale.
Effective DFM comments go beyond stating 'manufacturable.' Reviews must annotate risk locations — including traces/holes, pads, coverlay openings, stiffener boundaries, outline tolerances, connector-end thickness, bend zones, and assembly clearances — and provide modification suggestions, responsible parties, and closure status.
Minimum line width/spacing or minimum hole size reflect capability limits only — they do not guarantee suitability for large-panel, fine-pitch, high-yield projects. The FPC manufacturer must further define the practical manufacturing window based on material selection, panel size, panelization method, process compensation, and target yield.
3. Material and stack-up solutions must serve the application.
PI film, copper foil, adhesive system, coverlay, stiffeners, and surface finish collectively influence thickness, flex stiffness, solderability, thermal resistance, and dimensional stability. For dynamic bend zones, focus on copper type, trace orientation, bend radius, and stiffener transition; for connector and solder areas, emphasize end thickness, planarity, and localized support.
Material part numbers, thicknesses, lot numbers, substitution rules, and change-approval procedures must be explicitly defined in project documentation. Unassessed material substitutions — even if electrical functionality passes in samples — must not enter mass production.
4. Sample approval does not equal mass-production reliability.
Engineering samples primarily validate design intent, dimensions, and mechanical fit; pilot runs verify process repeatability; mass production validates yield, cycle time, inspection coverage, and batch-to-batch consistency. These three phases have distinct objectives — one successful sample result cannot replace full-stage evaluation.
If samples undergo manual edge trimming, temporary stiffening, selective sorting, or rework, such deviations must be documented in the report. Customers need to know which results are scalable to planned production lines and which represent one-time engineering interventions.
5. Process quality must intercept issues at intermediate checkpoints.
Incoming material, drilling, patterning, plating, coverlay lamination, stiffener bonding, routing, electrical test, and final shipment each require dedicated process controls. AOI and 100% electrical testing are critical but insufficient substitutes for material lot verification, dimensional checks, assembly validation, visual inspection, and reliability testing.
Upon anomaly detection, the manufacturer must first tag and quarantine affected raw materials, work-in-process, and finished goods — then define scope using equipment logs, work orders, timestamps, material lots, and inspection data. Isolating only the few identified units does not confirm resolution of broader batch risk.
6. Reliability validation must mirror real-world assembly conditions.
Automotive programs typically require integrated validation plans covering temperature cycling, vibration, flexing, damp heat, soldering, and functional assembly. Robotics programs further specify motion radius, stroke length, direction, frequency, torsion, and target lifetime. Starry-sky-ceiling automotive FPCs demand special attention to large-panel handling, curved-surface conformability, LED placement accuracy, seam interfaces, lamination yield, and SMT compatibility.
Reports must document sample revision, material lot, tooling used, test conditions, sample size, monitoring methodology, and failure criteria. A generic statement of 'test passed' provides no insight into risk coverage.
7. Delivery timelines must reflect process milestones — not just a blanket 'X-day lead time'.
True delivery cycles include drawing freeze, DFM completion, material availability, engineering build, first-article inspection, testing, customer approval, production scheduling, and shipment. An FPC manufacturer offering only an unconditional number of days makes it difficult for procurement to assess applicability to your specific product.
During RFQ, simultaneously confirm sample quantity, production volume, specified materials, special surface finishes, test items, reporting requirements, and current production loading. Expedited orders may reallocate resources — but must never skip reviews, reduce inspections, or unilaterally substitute materials to meet nominal deadlines.
8. Traceability and change management determine long-term partnership risk.
Mass-production records must link drawing revisions, material lots, production work orders, critical process steps, inspection results, rework history, packaging labels, and shipment batches. Automotive and robotics programs additionally require defined sample retention, exception-response protocols, and formal change notifications.
Any changes to materials, processes, equipment, subcontractors, or inspection methods must undergo risk assessment, customer notification, sample confirmation, and revalidation where necessary. Without formal change control, even initially qualified samples may gradually drift out of specification across subsequent batches.
What else to evaluate by application:
For electronic shifter FPC manufacturers:Prioritize dynamic bending performance, connector-end robustness, vibration resistance, intermittent-break monitoring, and automotive assembly validation.
For robotics FPC manufacturers:Prioritize 3D motion envelope compliance, joint/dexterous-hand zone segmentation, dynamic lifetime validation, signal integrity assurance, and batch-replication capability.
For automotive flexible circuit board manufacturers:Prioritize thermal/vibration performance, material lot consistency, process quality control, and automotive-grade traceability.
For robotics FPC and dexterous-hand FPC projects:Prioritize confined-space routing, high-density sensing integration, stiffener boundary precision, and real-motion functional validation.
For automotive starry-sky-ceiling FPC projects:Prioritize large-panel handling, curved-surface conformability, LED pixel placement accuracy, seam interface design, lamination yield, and SMT process compatibility.
When issuing RFQ packages to FPC manufacturers, include these items upfront:
Provide controlled versions of Gerber files, schematics, BOMs, stack-up drawings, material/copper thickness specs, surface finish requirements, stiffener details, 3D mechanical structures, connector specifications, mounting point definitions, bend-use-case descriptions, temperature/vibration profiles, current/impedance requirements, sample quantities, forecasted volumes, delivery milestones, and acceptance criteria.
The more complete the package, the better the manufacturer can deliver comparable proposals for DFM, material selection, process planning, test strategy, and pricing — and the earlier true project risks can be identified prior to first-article build.
What Hongyi Precision offers:
Dongguan Hongyi Precision Circuit Co., Ltd. supports automotive electronics, humanoid robotics, dexterous hands, automotive starry-sky ceilings, and consumer electronics projects with FPC and FPCA services including drawing review, DFM analysis, material and stack-up recommendations, engineering prototyping, assembly verification, reliability validation, and mass-production support.
Refer to application-specific pages for:Robotics FPC Manufacturers & Humanoid Robot Flexible Circuit Board Solutions,Dexterous-Hand FPC Products,Automotive Flexible Circuit Board Manufacturer Solutions,Electronic Shifter FPC Manufacturer ProductsandAutomotive Starry-Sky-Ceiling FPC Case Studies. Specific specifications, lead times, and validation results are subject to customer drawings, actual operating conditions, and mutually approved documentation.
Summary:A truly qualified FPC manufacturer is not the one advertising the most parameters or offering the lowest price — but the one capable of closing the loop across drawing interpretation, material selection, process execution, validation rigor, quality assurance, and delivery discipline — delivering evidence-based engineering solutions tailored to each application domain.